IATF 16949 in Production: How CNCTech Controls Quality


IATF 16949 in Production: How CNCTech Runs Its Quality Management System
In automotive component manufacturing, quality is not created at the final inspection stage. It is built throughout the process, from receiving customer requirements and setting production conditions to controlling deviations and tracing back when problems arise.
This is how CNCTech operates its IATF 16949 quality management system in molding and tooling production. IATF 16949 sets the framework and control principles. What makes it work is turning those requirements into concrete production activities, with clear responsibilities, standards, and control records across every department involved.
This article walks through four areas: requirements, in-process control, traceability, and deviation handling.
1. Receiving and Standardizing Customer Requirements
One of the first risks in automotive manufacturing is not on the shop floor. It is in understanding and translating product requirements.
Requirements review for every new part number
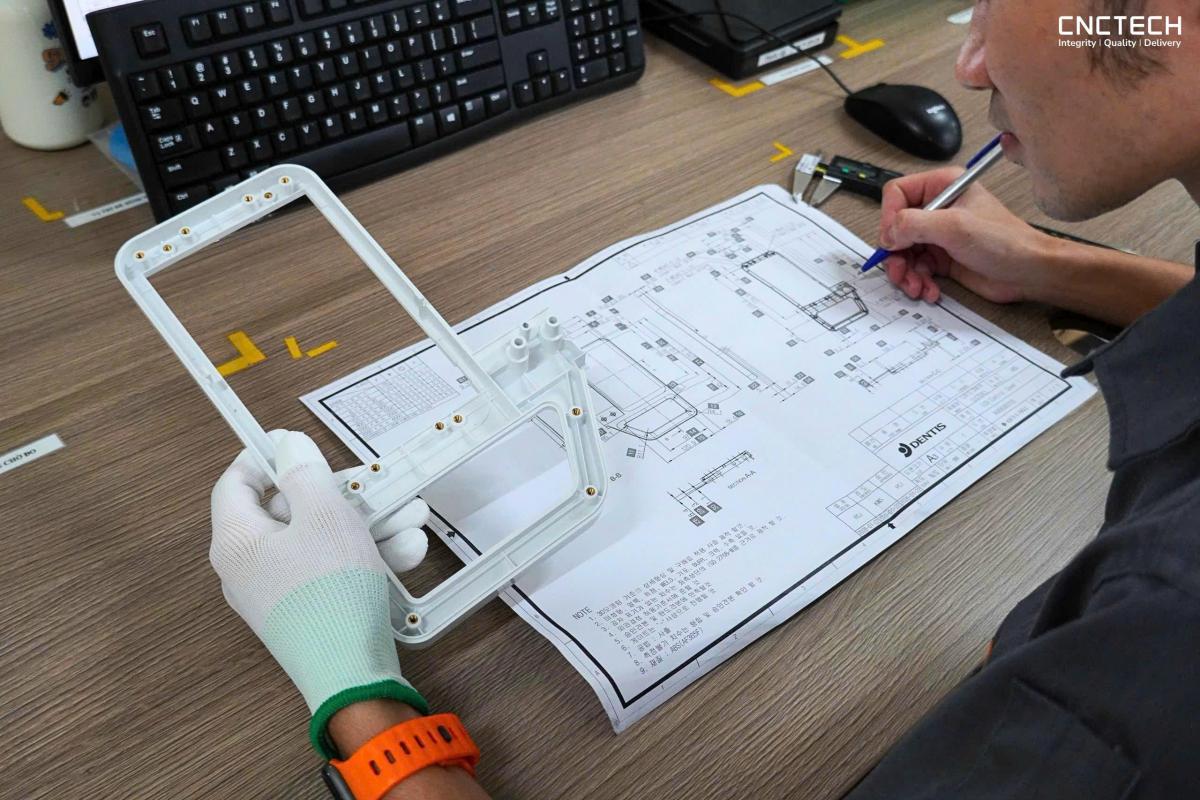
When CNCTech receives a new part number, the relevant departments review the drawings and customer requirements:
Dimensions and appearance
Materials and critical characteristics
Inspection standards
Packaging and labeling
Any special customer requirements
At the same time, the team assesses whether the molds, machines, equipment, and production conditions can meet those requirements.
Sample evaluation: APQP, PPAP, FMEA, Control Plan, SPC and MSA
The product is then trial-molded, inspected, and sent to the customer for evaluation. During this stage, CNCTech builds, reviews, and tracks the core automotive quality records: APQP, PPAP, FMEA, Control Plan, SPC, and MSA. All records are retained to support mass production.
Standardizing into controlled documents
After the customer approves the sample, the confirmed requirements become an internal controlled document system:
Process Flow
FMEA and Control Plan
Inspection standards
Work instructions
Checksheets
All documents are kept at the latest revision, and each department gets its own clear role:
Engineering sets up and controls production conditions.
Production follows the issued work instructions and standards.
QC inspects and controls according to the approved Control Plan, inspection standards, and Checksheets.
Before mass production begins, the departments reconfirm requirements, control documents, and production conditions. The goal is simple: an acceptable sample must never depend on individual experience or the chance conditions of one trial run.
2. In-Process Quality Control
Once requirements and conditions are confirmed, the task is to keep them stable throughout production.
Machine, mold and parameter verification
Before production starts, Engineering checks the molding machine, the mold, and the production parameters against the standards set during sample trials.
When a mold changeover happens, production conditions change, or an abnormality occurs, the related parameters and the first-piece product must be inspected and confirmed before mass production continues. These changes are recorded so they can be tracked in later runs.
QC monitoring during production
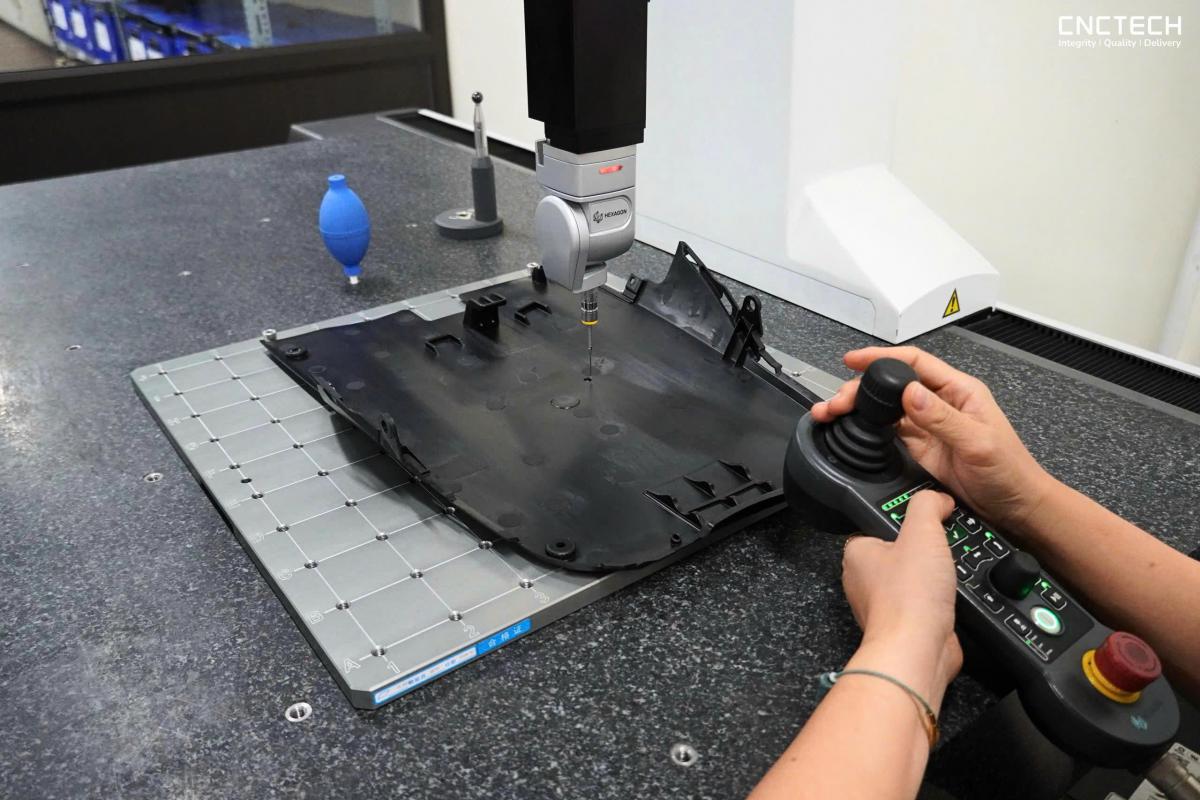
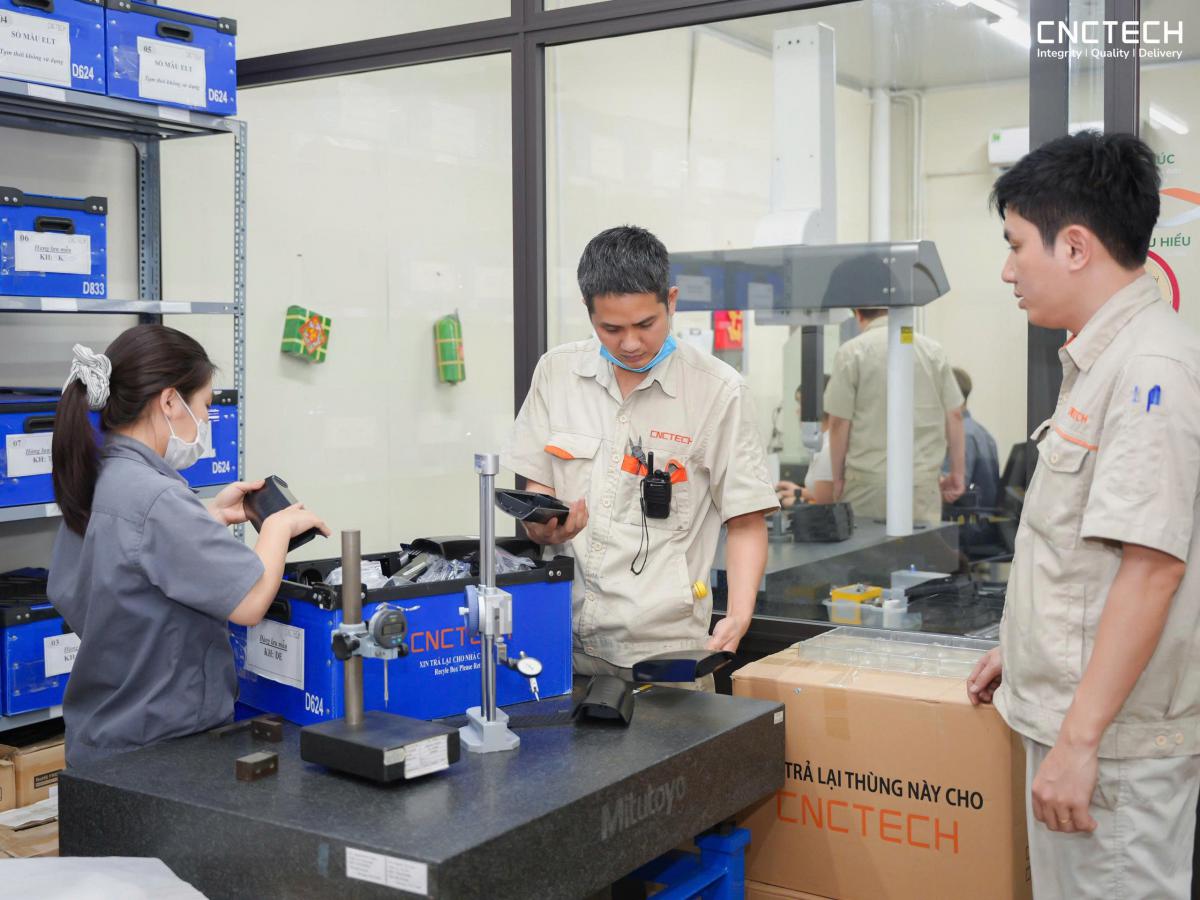
Start-of-shift inspection: appearance, dimensions, and critical characteristics checked against the standard for each part number.
Periodic QC patrol: in-process inspection following the Checksheet and the defined frequency.
Abnormality control: when a deviation is found, affected products are contained and handled per procedure before production continues.
Afterward, the relevant departments analyze the root cause, define countermeasures, and verify their effectiveness. Results are monitored to confirm the problem is resolved and to reduce the risk of recurrence.
3. Traceability Records
In mass production, traceability lets a plant determine under what conditions a batch was made, which materials it used, and which inspections it passed. At CNCTech, information is stored and linked by record group:
Record group | What can be traced | Source records |
Inventory | Stock quantity and status | System and consolidated inventory file |
Production history | Part number, LOT, production date, machine, shift | Production plan, finished-goods label, production records |
Raw materials | Material code, material LOT, supplier | Inspection and material control records |
Production process | Molding machine, settings, operators | Engineering and production records |
Quality inspection | IQC, PQC (appearance, dimensions), OQC final results | Records, Checksheets, inspection standards |
Shipment | Quantity, ship date, delivery note, receiving customer | Delivery and receipt records |
With this linkage, a batch can be reviewed across the whole chain, from raw material to production conditions to inspection results to shipment, instead of relying only on the final inspection result.
4. Handling Deviations and Verifying Effectiveness
When a quality issue is detected, CNCTech follows a fixed sequence:
Confirm the situation → Isolate and contain → Analyze root causes → Implement countermeasures → Verify effectiveness
Confirm and assess impact. The issue is verified and its scope evaluated.
Isolate and contain. Affected products are separated. Products from the same LOT or produced under the same conditions are also checked, so nonconforming (NG) products do not move to the next process or get shipped.
Analyze root causes. Teams analyze both the occurrence root cause and the escape root cause using 5 Why, 4M, and direct checks at the process.
Implement corrective and preventive actions. Short-term and long-term actions are applied. Inspection standards, work instructions, or Checksheets are updated when needed.
Verify effectiveness. Subsequent lots are monitored for recurrence and compliance. A countermeasure is confirmed effective only when results are satisfactory and the defect does not return.
What the System Is Designed to Deliver
IATF 16949 is not about adding more forms or checkpoints. It is about building a repeatable, evidence-based chain of control:
Requirements are understood correctly.
Production conditions are standardized.
Deviations are detected early.
Product history is traceable.
Problems that arise become data for the next production run.
In automotive mass production, the real challenge is not making one good batch. It is making sure the next batch, the next shift, and every run after that keeps the same level of control.
Frequently Asked Questions
What does IATF 16949 require in production?
It sets a framework of requirements and control principles for automotive quality management. In practice, these must be turned into clear activities, responsibilities, standards, and records, from requirements review and in-process control to traceability and corrective action.
Which documents does CNCTech prepare before mass production?
APQP, PPAP, FMEA, Control Plan, SPC, and MSA records are built during sample evaluation. After customer approval they become the Process Flow, Control Plan, inspection standards, work instructions, and Checksheets used in production.
How does CNCTech trace a product batch?
Records for inventory, production history, raw materials, production process, inspection results, and shipment are linked, so a batch can be traced from material LOT to shipment.
How does CNCTech confirm that a corrective action worked?
Subsequent production lots are monitored for recurrence and compliance. The countermeasure is confirmed effective only when results meet requirements and the defect does not repeat.
Talk to CNCTech About Quality in Mass Production
Working in Quality, Engineering, or Production? Which is hardest to control when keeping quality stable in mass production: change control, maintaining production conditions, LOT traceability, or verifying the effectiveness of countermeasures? CNCTech would like to hear your perspective and hands-on experience.
Contact information
Email: hello@cnctech.vn
Phone: (+84) 868 208 111
Corporate Website: https://cnctech.com.vn/
Manufacturing Technology Website: https://cnctech.com.vn/manufacturing
Linkedin: http://linkedin.com/company/cnctech-manufacturing-technology/
Tiktok: https://www.tiktok.com/@cnctechmanufacturing
Youtube: https://www.youtube.com/@cnctech-vn

Tin tức liên quan